
Introduction: Why Functional Labels Pose a New Problem for Prepress Research
Pharmaceutical packaging is shifting from a passive surface that carries information to an active interface involved in the treatment process, and labels are the most direct vehicle of this shift. The label Schreiner MediPharm developed for a weight-loss pen combines NFC authentication with a grip support structure, giving a single label dual roles: product identity verification and human factors support [1]. This design is not an isolated case. The same supplier developed an NFC label for Ypsomed's UnoPen injector pen back in 2021 [2]. Separated by several years, the functional scope expanded clearly between the two cases, offering a solid sample for observing the evolution of functional labels
The core research question of this article is: when a label takes on print, electronic, and structural functions all at once, are existing prepress file specifications, preflight inspection routines, and pricing structures still adequate?
Existing discussions leave a clear gap. Technical literature on Near Field Communication (NFC) tags focuses mostly on chip performance, read range, and anti-tampering mechanisms, while authoritative standards in prepress (such as the Ghent Workgroup, GWG) focus on print predictability and reliable file exchange [3][5]. Both tracks are mature on their own, but they rarely cross paths. The former does not address how files should be prepared and handed off to printers, while the latter does not address how antenna zones should be marked and protected on the layout. This article builds an analysis directly at this intersection
This article makes three contributions, each matching a subsequent section:
・First, tracing the evolution of functional NFC labels in pharmaceutical packaging, showing how the focus has expanded from pure anti-counterfeiting to authentication plus user behavior support (see 'Literature and Current State Review')
・Second, breaking down the specific impact of composite labels on prepress file architecture, proposing an analytical framework that expands traditional prepress checks into cross-disciplinary inspection (see 'Core Analysis 1 and 2')
・Third, offering actionable workflow and pricing recommendations across three levels: Taiwan's small and medium print shops, designers, and brand owners (see 'Implications for Taiwan's Design and Printing Industry')
For Taiwan, the significance of this topic lies in its industrial positioning. Taiwan's design and printing sector has long relied on commercial printing and general packaging, where gross margins are squeezed by raw material and labor costs. Medical-grade functional labels represent low-volume, high-specification orders with substantial verification costs. The barrier to entry does not lie in press machinery, but in process discipline and cross-disciplinary coordination. This analysis argues that this is precisely where existing printers can build differentiation through institutionalized processes rather than heavy capital expenditure
Literature and Current State Review: Divergences and Gaps Across Three Tracks
This section traces three related tracks, identifies where they diverge, and establishes the focus of this article
Track 1: NFC labels as pharmaceutical anti-counterfeiting tools. A representative case is the NFC label Schreiner MediPharm developed in 2021 for Ypsomed's UnoPen [2]. That project proved the technical feasibility of NFC on pen injectors: adding a digital identity without altering the physical structure of the device itself. Research in this track centers on whether the chip can be attached and whether it can be read. The difference here is that this article no longer treats feasibility as an open question. Taking feasibility as proven, it asks instead what demands this places on upstream prepress file creation
Track 2: Expanding the functional scope of NFC. The recent weight-loss pen case shows that beyond NFC authentication, the same label now incorporates grip support and anti-slip surface treatments [1]. This means the logic of functional integration has shifted from simply adding a chip to redesigning the label's entire physical and digital layer stack. The label is no longer just scanned. It is touched, gripped, and subjected to repeated mechanical force. Stacking these functions directly increases the number of prepress variables and serves as the empirical starting point for our core analysis
Track 3: Prepress file standard systems. The Ghent Workgroup has long maintained cross-industry prepress technical specifications, offering a common baseline for file exchange and predictable output [3][4][5]. The value of this system is turning the question of whether a file can print correctly into verifiable criteria. However, this analysis argues that such standards rest on the premise that the final output is strictly a printed image. Once a label incorporates antenna loops and zoned surface finishes, the checklist of verifiable criteria runs into blank spots. The standards are not wrong, they simply do not cover these aspects yet
The divergence among these three tracks is clear: technology suppliers have already stacked features into the third layer, while standard bodies still regulate only the first layer. A public operational framework that integrates electronic and structural layers into prepress verification criteria remains missing, and that is where this article steps in
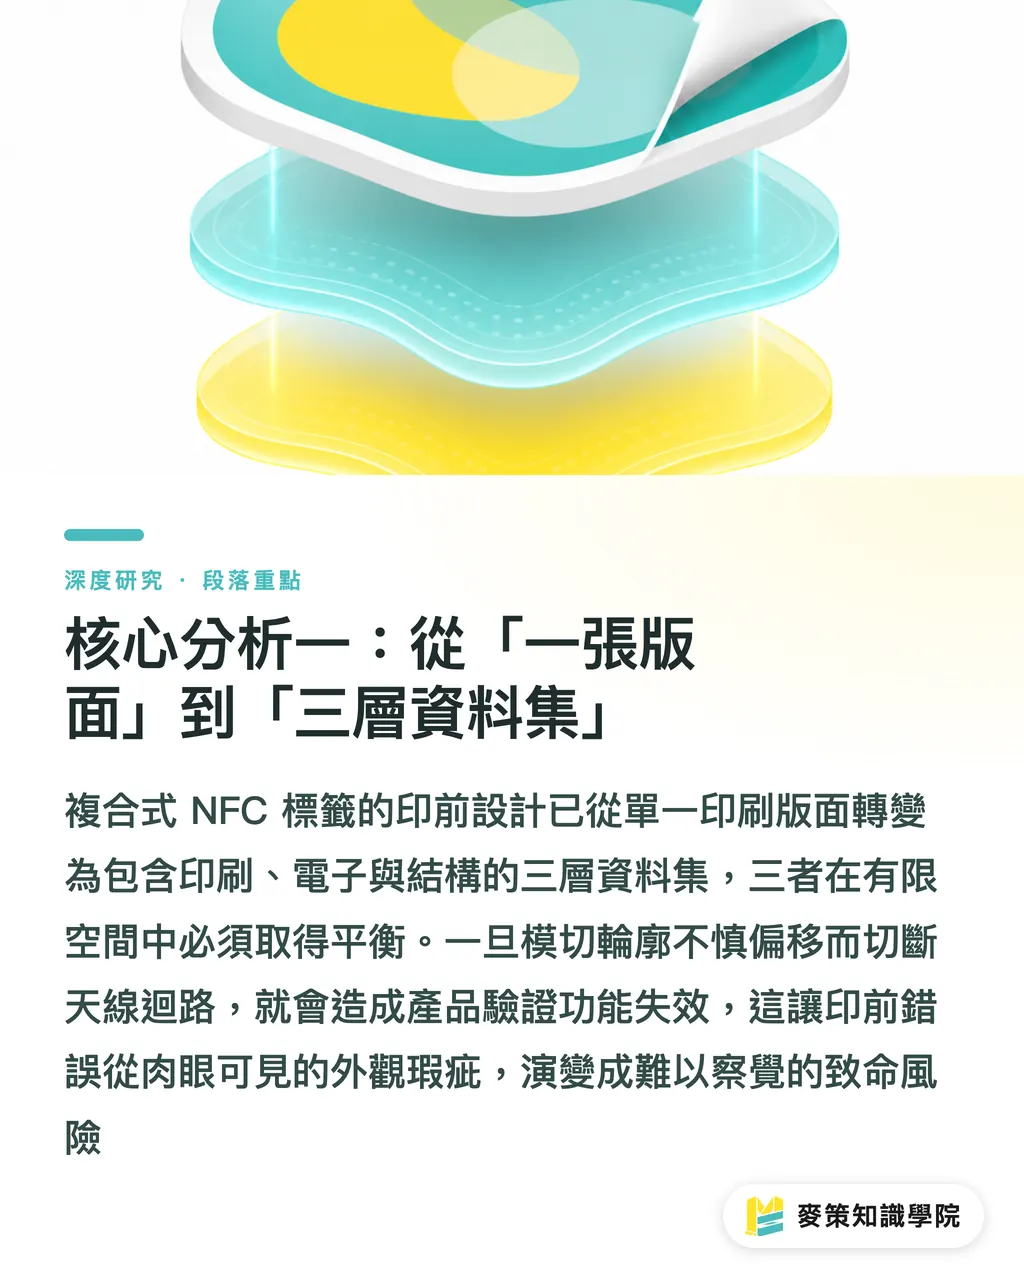
Core Analysis 1: From a Single Layout to a Three-Layer Dataset
The most fundamental change with composite NFC labels is the definition of the prepress deliverable itself
The deliverable in traditional label prepress is a print layout covering color, typography, bleed, overprint, and barcode readability. These elements all answer a single question: will the image land on the substrate as expected? The Ghent Workgroup specifications establish verifiable conditions around exactly these questions [3][5]. The completeness of existing standards has a clear boundary, which is that it applies only to the printed image
In the weight-loss pen case, the label carries two non-print functions: NFC anti-counterfeiting verification and grip support [1]. The same label surface must satisfy three competing optimization goals: the print layer demands graphic fidelity, the electronic layer requires unbroken antenna circuits, and the structural layer demands surface friction and tactile ergonomics. All three compete for the exact same physical space on the layout
This leads directly to a layered architecture for prepress datasets, which can be understood in three distinct layers:
・Print layer: Graphics, text, colors, mandatory regulatory markings, and legibility requirements
・Electronic layer: Antenna layout zones, chip placement, and keep-out areas where embossing, debossing, or cutting is prohibited
・Structural layer: Zoned anti-slip or tactile surface finishes, die-cut contours, and 3D deformation tolerances after application
Hard conflicts exist between these three layers. For instance, shifting a die-cut contour inward by a few millimeters due to a design adjustment is merely a trimming risk on a conventional label, but on an antenna-bearing label, it can sever the circuit and kill product verification. The nature of prepress errors changes as a result, shifting from a ruined print run to a label that looks flawless but fails functionally. Because visual inspection cannot catch this, the failure is far harder to detect
Public sources do not disclose antenna specifications, substrate layer counts, or production yields for this case. This analysis derives its points from the disclosed functional combination alone, without claiming specific engineering parameters
Core Analysis 2: Expanding Verification Criteria and the Three-Gate Methodological Framework
The second major impact of functional labels is that verification checkpoints must move upstream, shifting from the final printed sheet to file architecture and physical sample validation
Comparing the 2021 Ypsomed UnoPen case with the recent weight-loss pen case reveals a clear evolutionary path [1][2]. The former established the feasibility of adding NFC to a pen injector, while the latter merged authentication and ergonomic functions into a single label [1]. As functional stacking becomes a steady trend, workflows need a repeatable verification structure rather than ad-hoc patches for individual projects
To make this actionable, this article organizes prepress verification criteria into a named framework called the 'Mai Strategy 3-Gate Check.' This framework does not replace existing standards. Instead, it places traditional print checks and new cross-disciplinary checks side by side on a single checklist:
・Gate 1 (Print Accuracy): Color, fonts, bleed, overprinting, barcodes, and regulatory label legibility. This gate maps directly to the verification logic of existing prepress standards [3][5]
・Gate 2 (Functional Integrity): Verifying that antenna keep-out zones are clearly designated on dedicated layers, minimum safety clearances between die-cut lines and electronic components are defined, and finish zones align with grip surfaces
・Gate 3 (Use-Case Validation): Testing whether NFC remains readable after application to curved surfaces, verifying that the anti-slip finish holds up under repeated handling, and ensuring the label stays adhered throughout the device's operational lifespan
Gate 3 warrants special emphasis. A weight-loss pen is a patient-operated, repeatedly handled device where the label acts as the grip interface [1]. Verification must therefore take place on the final 3D assembled unit, not on flat press proofs. Traditional prepress workflows do not account for the gap between flat proofing and post-application functional testing
Gates 2 and 3 involve process and system design costs, covering dedicated layer naming conventions, cross-disciplinary clearance definitions, and sampling protocols for post-application read tests. Small and medium print shops can adopt these steps without investing in expensive capital machinery
Implications for Taiwan's Design and Printing Industry
This section outlines practical implications across three levels, with concrete details on workflows, costs, and timelines
For small and medium print shops. Competition for functional label orders does not hinge on unit price, but on the ability to handle cross-disciplinary collaboration. Three practical steps stand out:
・First, create file handoff specifications that include electronic and structural layers, explicitly requiring clients to provide dedicated antenna layers and minimum safety clearances. This is a one-time documentation investment
・Second, include post-application read testing as a standard line item in quotes rather than a free add-on, since it requires physical device samples and extra labor hours
・Third, separate print labor from validation labor in quotes to keep testing costs from eroding the print margin. This distinction is vital for maintaining profitability on these orders, as testing time carries far greater variance than press time
For designers. The easiest trap in design is underestimating invisible constraints. Conventional label design is bounded by margins and bleed, but functional labels carry unseen electronic zones. Practical recommendations include requesting antenna layouts from the client early on and building non-printing reference layers directly into the design files, avoiding heavy ink coverage or metallic finishes over antenna areas, and aligning surface finish zones with ergonomic grip points rather than purely visual balance [1]. Design freedom is constrained on these projects, but building limitations in at the concept stage is far cheaper than catching them during proofing
For brand owners and medical device manufacturers. The choice to adopt NFC labels should not focus solely on anti-counterfeiting benefits. It must account for downstream data governance and project schedules. Actionable evaluation points include determining who manages the landing content after scanning, how regulatory copy is divided between physical print and digital content across markets, and what backup identification exists if a tag fails. In terms of scheduling, functional label projects require extra round-trips for sample application and scan testing compared to standard print runs. Teams should allocate a dedicated schedule buffer for this rather than rolling it into standard proof approval
Conclusion and Limitations
This article addresses the question raised in the introduction: when a label handles print, electronic, and structural functions simultaneously, existing prepress workflows fall short. The weight-loss pen case shows that NFC authentication has merged with ergonomic features like grip support on a single label [1], following a clear expansion of functions since the 2021 Ypsomed UnoPen case [2]. Current prepress standards focus on print accuracy, and their verifiable criteria do not yet cover antenna keep-outs or surface treatment zoning [3][5]. This article puts forward a three-layer dataset framework and the 'Mai Strategy 3-Gate Check' protocol, translating them into specific practices for three industry roles in Taiwan
Two specific limitations should be clearly stated
First, limited source data coverage. The primary evidence available here covers only two cases from a single vendor. Public information on the weight-loss pen case remains limited to functional descriptions [1], without disclosing antenna specifications, material stack-ups, production yields, or cost figures. All prepress impacts derived in this article represent mechanistic analysis rather than empirically verified engineering conclusions. Readers should not treat them as technical specifications for any specific product
Second, boundaries on generalization. This analysis focuses on small, curved labels on pen injectors. These products feature high unit prices, low production volumes, and strict regulatory requirements, allowing product margins to absorb testing costs. Extrapolating these conclusions to food packaging, consumer goods, or large-format flat packaging breaks the underlying assumptions about cost structures and inspection intensity, requiring separate evaluation
Future research can proceed along three lines:
・First, collecting functional label cases across multiple vendors to test whether the three-layer dataset framework holds up across different applications
・Second, conducting workflow surveys in Taiwanese print production environments to quantify the actual labor hours and sampling rates needed for post-application read testing
・Third, benchmarking against the clause structures of existing prepress specification documents [3][5] to draft field definitions for incorporating electronic and structural layers into standardized preflight checks
Key Takeaways
・Schreiner MediPharm's weight-loss pen label integrates NFC authentication with grip support, showing how medical labels have shifted from simple anti-counterfeiting accessories into composite print, electronic, and structural components [1]
・The prepress deliverable for functional labels is no longer a single print layout, but a three-layer dataset comprising the print layer, electronic layer (antenna keep-outs), and structural layer (finish zones)
・Prepress errors on antenna-bearing labels carry different consequences than traditional jobs: defects may look visually normal while failing functionally, rendering visual inspection useless and requiring post-application 3D testing
・For Taiwanese small and medium printers, the barrier to taking on these orders is process discipline rather than capital investment, with the key being separating validation labor from print pricing
・Current prepress standard systems center on print accuracy [3][5] and do not yet cover cross-disciplinary parameters, creating an opportunity for the industry to build verifiable operational standards
Further Considerations
Functional labels push print shops into unfamiliar territory, requiring them to deliver a testable function rather than just printed output. For print manufacturing, the most pragmatic next step is institutionalizing file handoff specs alongside post-application read testing, while pricing validation labor separately in quotes. Otherwise, hidden labor hours will eat up margins on high-spec jobs. On the design side, antenna layout files should enter reference layers during early conceptual work just like brand guidelines, preventing hidden constraints from surfacing late in proofing. The sensible entry point for AI is not layout generation, but automated preflight checks. Rule-based checks can detect clearance violations between electronic zones and die-lines, missing layer names, or misalignments between surface finishes and grip zones. These tasks have clear parameters, can be automated, and carry high error costs. On the SaaS side, building shared collaboration spaces around cross-disciplinary checklists could allow brands, designers, label suppliers, and printers to maintain versioned records against a single spec. Many open issues remain: there is still no common standard across suppliers for marking antenna zones, and public benchmarks for post-application read test sampling rates do not exist yet. These two gaps will determine whether such orders can move from custom one-off projects to scalable standards
References
[1] NFC labels enter healthcare: Weight-loss pens get 'talking labels'
[2] Schreiner MediPharm develops NFC label for Ypsomed's UnoPen. OPE Journal. DOI: 10.51202/2366-8040-2021-35-006
[3] Ghent Workgroup: GWG Technical Specifications Home. Ghent Workgroup
[4] Ghent Workgroup: GWG Official Home. Ghent Workgroup
[5] Ghent Workgroup: GWG Specifications Overview. Ghent Workgroup
FAQ
- What practical functions do NFC labels serve on weight-loss pens?
- The label Schreiner MediPharm developed for weight-loss pens provides both NFC anti-counterfeiting authentication and grip support. The former verifies product authenticity, while the anti-slip surface improves user handling ergonomics [1]. This makes the label both a verification portal and an active user interface
- What additional prepress steps must print shops take when handling functional NFC labels?
- At least two new types of checks are needed. First, marking antenna keep-out zones on dedicated file layers and defining minimum safety clearances to die-cut lines. Second, testing NFC readability after applying the label to actual curved device surfaces. Passing flat press proofing does not guarantee functional success in production
- Why are prepress errors on antenna-bearing labels more dangerous than on conventional labels?
- Because errors can manifest as products that look normal but fail functionally. Shifting a die-cut line inward by a few millimeters on a conventional label is merely a trimming risk, but on an antenna-bearing label it can sever the circuit and break authentication. Visual inspections cannot detect this kind of failure
- Can existing prepress standards like Ghent Workgroup be applied directly to functional labels?
- They cover print accuracy, but cannot cover the entire scope. Existing prepress standards focus on print predictability and reliable file exchange [3][5], leaving out verifiable criteria for antenna keep-out zones and surface finish zoning. Printers must establish their own supplementary specifications for these areas
- What is the primary barrier for Taiwanese small and medium printers entering medical functional label production?
- The primary barrier is process discipline and cross-disciplinary coordination rather than printing equipment. Key investments include file handoff specifications, documented cross-disciplinary safety clearances, and pricing models that separate validation labor from print rates
Related articles
The Print × AI weekly
The print and AI know-how designers, brands and enterprises can use before they commit — one email, every week
MINDS Free Tools
Imposition calculator and preflight file check — free prepress tools, right in your browser.
MINDS Group
Need actual printing or gifting services?
From premium printing to online ordering and festive gifts — the MINDS Group sister brands take it from here.