
Introduction: Why a Commercial-Scale Pilot Run Deserves Scholarly Scrutiny
Packaging print decarbonization narratives have long focused on substrates and binders. Progress on replacing colorants has been comparatively thin, making any industrial-scale bio-based colorant pilot significant. In August 2026, Tampere University of Applied Sciences (TAMK) led Natural Indigo Finland, BioInk, Meira, Siegwerk, and Hornung Verpackungen in successfully printing cross-bottom bags with water-based ink formulated from colorants extracted from coffee-roasting side streams [1]. The project began with laboratory research two years earlier, completed a flexographic printing validation on fiber-based shopping bags in 2025, and entered commercial scale in 2026 [1]
Here, the core terms used in this article are defined first and kept consistent throughout. Flexography refers to printing that transfers low-viscosity ink using a flexible relief plate and anilox roll. It is a mainstream process for paper bags and flexible packaging. Water-based ink refers to an ink system that uses water as its primary solvent carrier and can significantly reduce volatile organic compound (VOC) emissions compared with solvent-based ink. Colorant refers broadly to the dye or pigment component that provides color. It serves a different function from the binder and varnish, which provide film formation and adhesion. A side stream refers to a material flow in an industrial process that would otherwise be sent to energy recovery or waste treatment
There are three gaps in existing discussions:
・First, research and commercial discussions on sustainable inks have long focused on the recycled content of binders, while the colorant side has been treated as a secondary variable. Siegwerk has also publicly stated that "sustainable ink development often focuses on recycled binders, while coffee-derived colorants fill a missing piece" [1]
・Second, academic literature on water-based flexographic inks generally discusses printability and substrate pretreatment on the assumption of synthetic pigments, and has yet to establish a corresponding quality-parameter framework for bio-based colorants [5]
・Third, although the deinking challenges of paper products containing flexographic ink have been documented in dedicated research, the innovation narrative around circular inks rarely circles back to test how they perform in recycling streams [3][4]
This article makes three contributions, each corresponding to a section of the main text:
・First, it reconstructs the technical chain from coffee by-products to flexo paper bags and uses flexographic printability literature to identify the quality parameters that still require validation, corresponding to Section 3
・Second, it places this case within the compliance framework established by the EU PPWR and analyzes how institutional demand can pull the commercialization of bio-based colorants ahead of technical maturity, corresponding to Section 4
・Third, using recycling-end compatibility as its axis, it identifies the closed-loop risk most often overlooked in circular-ink narratives, corresponding to Section 5. This issue matters to Taiwan because its paper-bag and flexible-packaging supply chains rely heavily on exports and contract manufacturing. Compliance thresholds under EU packaging rules will flow back through the supply chain to local small and medium-sized printers, while most operators have yet to establish auditable process-data baselines
Literature and Current State of the Field: Three Research Strands That Rarely Speak to One Another
Existing research falls into three clusters with little overlap. That gap is where this article begins
The first cluster concerns flexographic printability and quality measurement. Related studies use Solid Ink Density (SID) as a core indicator to compare the performance of the same flexographic process on different print media, including Polypropylene (PP), Polyethylene (PE), and chromo paper [2]. Other research examines water-based flexographic printing on polymer-coated paperboard and considers how print quality and resistance depend jointly on ink formulation and substrate pretreatment [5]. This cluster establishes a key premise: flexographic quality is not determined by ink alone but by the coupled result of ink formulation and substrate surface conditions [5]. We therefore point out that the performance of the coffee-colorant ink in this pilot applies only to fiber-based substrates such as paper bags and cannot be transferred directly to other materials
The second cluster concerns problems caused by flexographic ink at the recycling end. In 1996, researchers proposed new deinking chemistry for mixed waste paper contaminated with flexographic ink, showing that the difficulty of separating flexographic ink in the recovered-paper stream is a long-documented issue [3]. A 2012 study examined the adsorption of flexographic ink by inorganic particles modified with cationic polymers, offering another treatment route within the same problem area [4]. The two studies, sixteen years apart, still address similar separation challenges. In our analysis, that time span itself shows that the deinkability of flexographic ink remains an unsolved problem. The relevance to this article is that the legitimacy of any new ink system marketed as circular should extend to validation at the recycling end, rather than stop at the reuse of by-products at the raw-material end [3][4]
The third cluster concerns packaging regulation and life-cycle assessment. The EU Packaging and Packaging Waste Regulation (PPWR) has been published in full on EUR-Lex and provides a unified legal basis for packaging design and recyclability within the EU [7]. The European Commission's Directorate-General for Environment also maintains a packaging-waste policy page that serves as an entry point to the policy context [8]. Meta-analysis literature on Life Cycle Assessment (LCA) in packaging has also accumulated in academic bibliographic systems, indicating that methods for cross-study comparison have been developed over time [9]. The difference from this article is that regulatory and LCA literature addresses the packaging system as a whole rather than substitution benefits at the colorant level. It therefore cannot directly answer the question, "What is the net environmental benefit of replacing synthetic pigments with coffee by-product colorants?"
The gap among the three clusters is therefore clear. Printability literature does not discuss bio-based colorants, deinking literature does not discuss new ink systems, and regulatory and LCA literature does not discuss the colorant layer. This article brings the three strands together to examine where the coffee-colorant ink is supported by evidence and where it remains unverified
Breaking Down the Technical Chain: From By-Product to Printable Water-Based Ink
The technical chain of coffee-colorant ink can be divided into four stages, each with its own conditions for success or failure
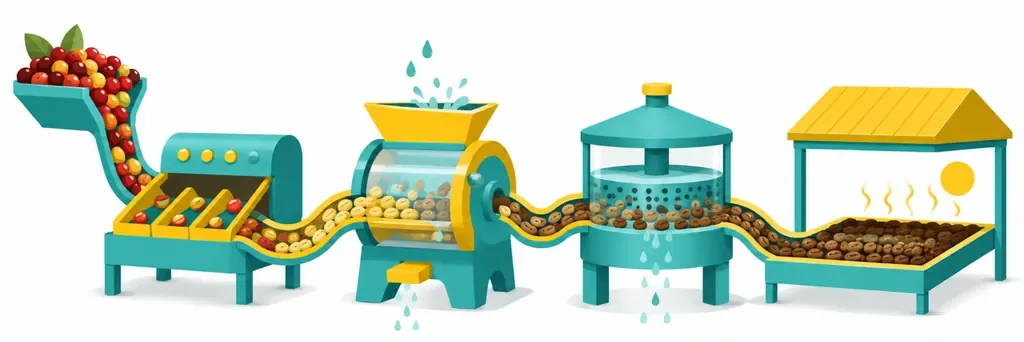
The first stage is raw-material supply. The colorant source is coffee-industry side-stream material supplied by Meira Oy. These materials originally went to energy recovery and were redirected through this route into higher-value renewable resources [1]. The key data point here is the statement that they originally went to energy recovery. Its significance is that the environmental baseline for this case is not landfill or incineration, but a material flow that already had energy-recovery value. Net benefits must therefore subtract the forgone energy-recovery value rather than be overestimated through the intuitive story of "turning waste into gold" [1]. As this analysis shows, marketing language often causes such cases to overlook this accounting detail
The second stage is colorant conversion and ink formulation. Natural Indigo Finland's BioInk technology converts the by-products into colorants, after which Siegwerk formulates them into industrial water-based printing ink [1]. The ink system produces no VOC emissions and uses a technical varnish with high bio-renewable content as its binder [1]. The claim "produces no VOC emissions" deserves precise interpretation. It means that the ink system has clear advantages in occupational hygiene and air-pollution compliance, but this is a general property of water-based ink systems, not an added benefit from the coffee colorant itself. It should therefore not be counted as an independent contribution of colorant substitution [1]. We believe that separating general ink properties from the colorant's innovative contribution helps evaluate this kind of innovation more rigorously
The third stage is printability validation. In 2025, the project completed flexographic printing validation on fiber-based shopping bags. In the commercial-scale pilot printing of cross-bottom paper bags in August 2026, it achieved good print quality, process compatibility, and performance under production conditions [1]. During this period, TAMK's Biocolores research group and its industrial partners continued improving color strength and technical performance to support more demanding packaging applications [1]. The statement "continued improving color strength" should be read as follows: insufficient color strength is a structural weakness of bio-based colorants, since chromophores from natural sources generally have lower molar extinction coefficients and lightfastness than synthetic organic pigments refined over decades. This also explains why the technology first moved into paper bags rather than high-end printing applications [1]
The fourth stage is measurement and standardization. Literature comparing flexographic quality uses Solid Ink Density (SID) as a core indicator and shows systematic differences in SID performance when the same process is used on different substrates [2]. The significance for this article is that if coffee-colorant ink is to move from paper bags to plastic substrates, SID and related printability tests must be rerun. Paper-bag data cannot simply be reused [2][5]. In our analysis, what bio-based colorants lack to move from a demonstration case to a standardized product is a public set of measurement data covering different substrates and batches
Institutional Drivers: How the PPWR Turns Colorant Substitution from a Bonus into a Requirement
Regulatory pressure, rather than a simple breakthrough narrative, is the key to understanding the commercial logic of this case
The full legal text of the EU Packaging and Packaging Waste Regulation (PPWR) has been published on EUR-Lex, providing a unified regulatory basis for packaging design, recyclability, and waste management within the EU [7]. The European Commission's Directorate-General for Environment packaging-waste page explains the position of packaging waste in EU environmental policy and outlines the relevant policy tools [8]. The significance of this institutional background is that once recyclability and hazardous-substance restrictions are written into directly applicable law, every material layer on packaging, including the ink layer, may become subject to compliance review. Colorant selection therefore shifts from a marketing bonus to a supply-chain risk-management issue [7][8]
The structure of the participants in this case supports that judgment. The pilot brought together an academic institution, TAMK, colorant technology developers, Natural Indigo Finland and BioInk, a raw-material supplier, Meira, a global ink manufacturer, Siegwerk, and a paper-bag converter, Hornung Verpackungen [1]. In our analysis, this cross-value-chain structure is not a natural form for a research project. It is typical of compliance-driven innovation. Because regulatory responsibility is distributed across the entire chain, validation must be carried out across the entire chain as well
External recognition of the innovation also provides a market signal. Coffee-ink packaging won public votes in the New Wood 2025 competition and the PacTec sustainable innovation competition in Helsinki, and received several international nominations [1]. Such awards should be interpreted carefully. Public voting reflects narrative appeal rather than the strength of technical validation. It can serve as an early indicator of brands' willingness to adopt the solution, but it does not constitute evidence of technical maturity [1]
The engineering challenges of paper bags as a packaging format are not new. As early as 1958, discussions addressed how stretchable paper could be used to make better bags, showing that the strength and formability of paper bags have long been research topics in paper packaging [6]. This historical depth reminds us that replacing plastic bags is constrained by mechanical performance. Innovation on the ink side cannot compensate for physical limits on the substrate side, and the two must be evaluated separately [6]
Closed-Loop Risk: The Least-Examined Link in Circular Inks
Circular-economy claims must close at the recycling end, and that is where the evidence is thinnest in this case
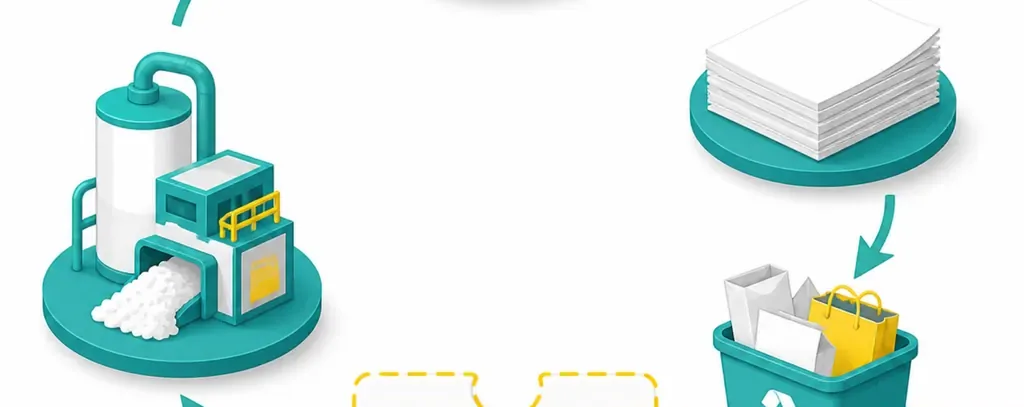
Existing literature clearly documents the difficulty of separating flexographic ink in recovered-paper streams. A 1996 study proposed new deinking chemistry specifically for mixed waste paper contaminated with flexographic ink [3]. A 2012 study examined the adsorption of flexographic ink by inorganic particles modified with cationic polymers [4]. The existence of these studies is itself evidence that the deinkability of flexographic ink has long been treated in the paper industry as a problem requiring specialized chemical treatment [3][4]. The significance for this article is that even if a new flexographic ink is made entirely from by-products at the raw-material end, its circular claim has completed only the first half if it creates equal or greater separation costs during deinking
The primary-source account of the coffee-colorant ink focuses on print quality, process compatibility, no VOC emissions, and a bio-renewable binder [1]. It does not mention deinkability or recycling-stream test results. In our analysis, this is a limitation of the reporting scope, not proof of a technical defect. Until public data become available, however, recyclability should be treated neutrally. We should not assume that it is better or worse than that of existing water-based flexographic inks
A further analytical consideration is that bio-based colorants may behave differently from synthetic pigments at the recycling end. Deinking strategies for synthetic organic pigments are largely built on established knowledge of particle size and interfacial properties [4]. Naturally sourced colorants, if they exist in dye form, may have water solubility that changes the separation mechanism. This is an inference in this article, not a literature conclusion, and requires empirical validation
This article therefore proposes a practical evaluation criterion: technical documentation for any ink innovation centered on the claim of being circular should include both printability data and recycling-stream compatibility data. Without the latter, a circular claim is an incomplete compliance argument in an environment where the PPWR has made recyclability a legal requirement [7]
Implications for Taiwan's Design and Printing Industry
Most players in Taiwan's printing supply chain will not develop bio-based colorants, but they will be the ones audited. That determines a sensible response. The following guidance is organized by role
For small and medium-sized printers, the feasible short-term move is not to buy bio-based ink, but to establish a process-data baseline:
・Create records of Solid Ink Density (SID) measurements for water-based flexography and store them by substrate. Flexographic quality is the coupled result of ink and substrate pretreatment, so data without substrate classification cannot support an audit response [2][5]
・Record the substrate pretreatment conditions for every batch, including surface tension and coating type. These are known key variables behind differences in water-based flexographic quality on polymer-coated substrates [5]
・Include VOC-emission status in routine records, because the no-VOC characteristic of water-based ink systems is a compliance asset that can be directly quantified and reported [1]
・In terms of timing, our analysis considers building a SID and pretreatment baseline covering three to five commonly used substrates an internal task that can be completed within several weeks to a quarter. The main cost is measurement labor, not equipment investment
For designers, the key is to move color decisions forward into the material-selection stage:
・Because the color strength of bio-based colorants is still being improved, design teams should not assume they can reproduce highly saturated colors or large-area solid color blocks [1]
・A design language built around a limited palette, linework, and whitespace has greater tolerance for bio-based colorant ink systems. This is an inference based on the color-strength limitation discussed above
・At the proofing stage, specify the substrate and ink system together. This avoids color disputes caused by using synthetic pigments for proofing and bio-based ink for production [5]
For brand owners, the quality of the audit questions matters. Our analysis suggests using Mai Strategy's Three-Gate Print Handoff Check to handle the introduction of sustainable materials. The first gate confirms the material's compliance position, including whether it falls within the PPWR's recyclability requirements [7]. The second confirms process reproducibility, including whether cross-batch printability data exist [2][5]. The third confirms recycling-end compatibility, including whether deinking or recycling-stream test data exist [3][4]. The third gate is the item most often missing from sustainable ink proposals today
Conclusion and Limitations
The research question in this article is how far the pathway from coffee by-products to flexographically printed paper bags is technically and institutionally viable. The answer has three layers. Technically, commercial-scale pilot printing of fiber-based paper bags achieved acceptable print quality and process compatibility under production conditions, so that part is empirically established [1]. Institutionally, the unified regulatory framework established by the PPWR provides clear commercial pressure for this kind of colorant substitution, so that part is structurally established [7][8]. Recycling-end compatibility lacks public data and remains unverified. Existing deinking research shows that this is not an area where optimism can be assumed [3][4]
This article has two specific limitations that must be disclosed
The first is the limitation of data timing and source coverage. First-hand information about the coffee-colorant ink is concentrated in a single industry-media report published on September 4, 2026 [1]. That report does not provide measurable parameters such as color-strength values, printing speed, anilox-roll specifications, lightfastness tests, or cost structure. The assessment of technical maturity in this article can therefore remain only qualitative and cannot support a quantitative comparison with similar ink systems
The second is the boundary of inference. The flexographic printability literature cited here studies synthetic-pigment ink systems [2][5], while the deinking literature examines the flexographic ink formulations available at the time [3][4]. Neither uses bio-based colorants as its sample. The two claims derived from these sources, that cross-substrate testing must be repeated and that the recycling end requires validation, are therefore risk warnings rather than confirmed defect findings
Future research has three actionable directions:
・First, measure Solid Ink Density (SID) across substrates for coffee-colorant water-based flexographic ink, covering kraft paper for paper bags, chromo paper, and polymer-coated paperboard. Build a parameter table that can be compared with existing synthetic-pigment data [2][5]
・Second, put paper-bag samples printed with coffee-colorant ink through a standard deinking process and measure residual ink and brightness indicators. This would directly address the separation challenges identified in existing research on flexographic-ink deinking [3][4]
・Third, use packaging Life Cycle Assessment (LCA) methodology, set "originally destined for energy recovery" as the baseline scenario, and calculate the net environmental benefit of colorant substitution to avoid overestimation [1][9]
Key Takeaways
In August 2026, TAMK, together with Siegwerk, Meira, and other partners, completed a commercial-scale flexographic pilot run on cross-bottom paper bags using water-based ink formulated with colorants derived from coffee-roasting by-products
The ink system produces no VOC emissions and uses a binder with high bio-renewable content, but no VOC emissions are a general property of water-based ink and should not be counted as an innovation contribution from the coffee colorant itself
Flexographic print quality is the coupled result of ink formulation and substrate pretreatment. Successful validation on paper bags cannot be transferred directly to plastic or coated substrates
The difficulty of deinking flexographic ink in recovered-paper streams has been documented for decades. This case currently lacks public recycling-end compatibility data, so its circular claim has completed only the first half
For small and medium-sized printers in Taiwan, the best short-term investment is not purchasing bio-based ink but establishing substrate-specific SID and pretreatment data baselines to respond to compliance audits from brand owners
Further Thoughts
For printing manufacturers, the signal from this case is not "it is time to change inks," but "it is time to start keeping data." Once the PPWR turns recyclability into a legal requirement, supply-chain audits will travel from brand owners back to contract manufacturers. Whether a supplier can promptly provide substrate-specific SID, pretreatment conditions, and VOC records will directly determine whether it can secure EU export work. For the design side, the color-strength limits of bio-based colorants mean that color decisions must move forward into the material-selection stage, with design language shifting toward fewer colors and stronger use of linework. AI has a clear role here. Classifying printability data, detecting cross-batch drift, and generating audit documents are all rule-based, structured-data tasks suited to automation rather than reliance on the memory and experience of veteran press operators. The opportunity for SaaS lies in a "compliance data layer" that maps SID measurements, substrate specifications, ink claims, and regulatory clauses, allowing a small or medium-sized printer to produce the audit response a brand owner needs within hours. Two questions remain unresolved: how to verify the batch-to-batch consistency of bio-based colorants at an affordable cost, and who will build a public database of recycling-end compatibility, since no single vendor has an incentive to shoulder that responsibility alone
References
[1] From Coffee Side Stream to Ink to Flexo Print Paper Bags: A Sustainable New Pathway
[2] Shrivastav P., Sharma S. (2023). A comparative analysis of Solid Ink Density values on Polypropylene (PP), Polyethylene (PE), and Chromo Paper print media utilizing Flexography printing. International Journal of Recent Advances in Engineering and Technology. DOI: 10.65521/intjournalrecadvengtech.v12i1.716
[3] Sain M., Marchildon L., Lapoine M. et al. (1996). A novel chemistry to ink separation from mixed paper waste contaminated with flexo ink. Nordic Pulp & Paper Research Journal. DOI: 10.3183/npprj-1996-11-03-p157-163
[4] 정 영., 이 학., 김 진. et al. (2012). Adsorption of Flexography Ink on Inorganic Particles Patched with Cationic Polymer. Journal of Korea Technical Association of The Pulp and Paper Industry. DOI: 10.7584/ktappi.2012.44.5.008
[5] Rentzhog M., Fogden A. (2006). Print quality and resistance for water-based flexography on polymer-coated boards: Dependence on ink formulation and substrate pretreatment. Progress in Organic Coatings. DOI: 10.1016/j.porgcoat.2006.08.003
[6] Stretchable Paper Makes Better Bags. The Science News-Letter. DOI: 10.2307/3939094
[7] EUR-Lex: Full Text of the EU PPWR Regulation. EUR-Lex
[8] European Commission Directorate-General for Environment: EU Packaging Waste Page. European Commission Directorate-General for Environment
[9] Mendeley (Journal of Cleaner Production paper): Meta-analysis of Packaging Life-Cycle Assessment. Mendeley (listing a Journal of Cleaner Production paper)
FAQ
- Can printing ink made from coffee by-products really be produced at scale?
- In August 2026, Finland's TAMK, together with Natural Indigo Finland, BioInk, Meira, Siegwerk, and Hornung Verpackungen, used water-based ink formulated with colorants derived from coffee-roasting by-products to complete flexographic printing on cross-bottom paper bags, achieving good print quality and process compatibility. The technology had already been validated on fiber-based shopping bags since 2025
- Does coffee-colorant ink perform as well in color as conventional ink?
- There is still a gap. The research team continues to improve the ink's color strength and technical performance for more demanding packaging applications. This shows that insufficient color strength is a structural challenge for bio-based colorants. Designs should not assume that highly saturated, large-area solid color blocks can be reproduced
- Are paper bags printed with this ink easy to recycle?
- There is currently no public data that can answer this. The difficulty of separating flexographic ink in recovered-paper streams has been documented for decades, with dedicated deinking studies published in 1996 and 2012. Until empirical data are available, the recyclability of coffee-colorant ink should be treated neutrally
- What should Taiwanese printers do now?
- Prioritize establishing a process-data baseline instead of rushing to purchase bio-based ink. Record Solid Ink Density (SID), substrate pretreatment conditions, and VOC-emission status by substrate. This baseline is necessary for responding to supply-chain audits related to the EU PPWR
- What practical impact does the PPWR have on Taiwan's packaging supply chain?
- The PPWR provides a unified regulatory basis for packaging design, recyclability, and waste management within the EU. Because compliance responsibility is distributed across the entire supply chain, audit requirements from EU brand owners will flow back to Taiwanese contract manufacturers and printers. Every material layer, including the ink layer, may become subject to review
Related articles
The Print × AI weekly
The print and AI know-how designers, brands and enterprises can use before they commit — one email, every week
MINDS Free Tools
AI background removal, a LINE sticker maker, spine & imposition calculators — all free, right in your browser, no upload.
MINDS Group
Need actual printing or gifting services?
From premium printing to online ordering and festive gifts — the MINDS Group sister brands take it from here.